Industry Applications
Versatile activated carbon solutions for diverse industrial applications worldwide
Activated Carbon Applications
Our premium activated carbon products serve a wide range of industries with proven performance and reliability.
Water Treatment
Purification of drinking water, wastewater, and industrial process water with efficient organic contaminant removal.
Air & Gas Purification
Removal of VOCs, odors, and harmful gases from industrial emissions and indoor air environments.
Food & Beverage
Decolorization and purification of sugar, edible oils, beverages, and food additives.
Gold Recovery
High-grade activated carbon for efficient gold adsorption in mining and metallurgical processes.
Chemical Processing
Catalyst support, solvent recovery, and purification in various chemical manufacturing processes.
Pharmaceutical
High-purity activated carbon for pharmaceutical manufacturing and medical applications.
Application Solutions
Explore how our activated carbon products deliver results across key industries.
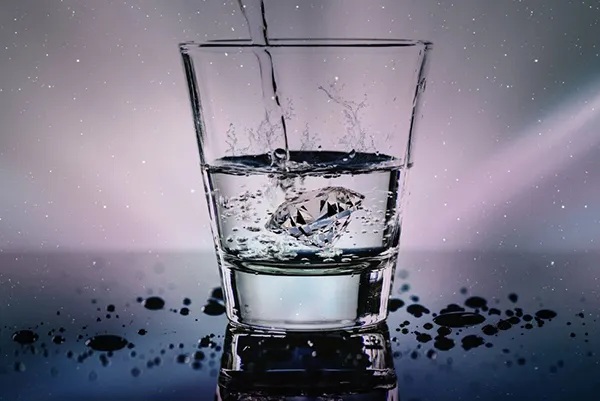
Pure Water Solutions for Every Need
Our activated carbon products are widely used in municipal drinking water treatment, industrial wastewater purification, and process water polishing. With high adsorption capacity for organic contaminants, chlorine, and odor-causing compounds.
- Municipal drinking water purification and taste/odor removal
- Industrial wastewater treatment and COD/BOD reduction
- Groundwater remediation and contaminated site treatment
- Process water polishing for electronics and power industries
- Swimming pool and spa water filtration systems
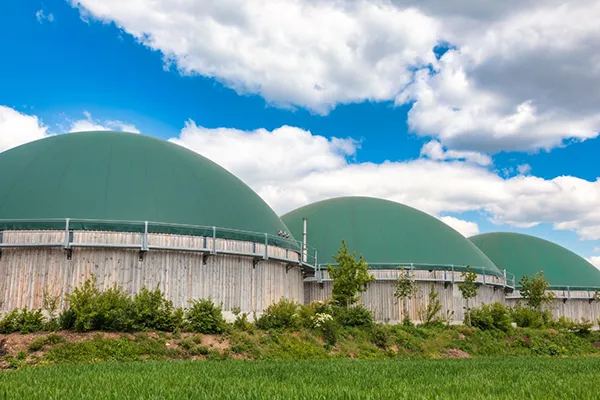
Clean Air for Healthier Environments
From industrial flue gas treatment to indoor air quality improvement, our activated carbon solutions effectively remove volatile organic compounds (VOCs), hazardous gases, and unpleasant odors from air streams.
- Industrial VOC removal and solvent recovery systems
- Flue gas treatment and sulfur dioxide removal
- Indoor air purification and HVAC filtration
- Automotive cabin air filters and emissions control
- Biogas purification and landfill gas treatment
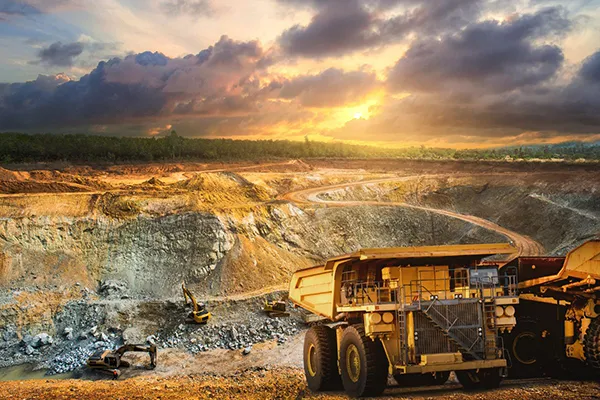
High-Efficiency Gold Adsorption Carbon
Our coconut shell-based activated carbon is specially optimized for gold recovery applications. With high hardness, excellent adsorption kinetics, and superior resistance to attrition, it's ideal for CIP/CIL gold mining operations.
- Carbon-in-Pulp (CIP) and Carbon-in-Leach (CIL) processes
- High hardness and attrition resistance for long service life
- Excellent gold loading capacity and elution properties
- Consistent particle size distribution for optimal flow
- Suitable for heap leach and Merrill-Crowe processes
Versatile Solutions for Chemical Industry
Activated carbon plays a crucial role in chemical manufacturing, from catalyst support to solvent recovery and product purification. Our products are engineered for consistent performance in demanding chemical applications.
- Catalyst carrier and support for chemical reactions
- Solvent recovery systems for cost-effective operations
- Chemical product purification and decolorization
- Petrochemical refining and hydrocarbon processing
- Wastewater treatment for chemical plants
Pharma-Grade Activated Carbon
Our pharmaceutical-grade activated carbon meets the strictest purity standards for use in pharmaceutical manufacturing. With ultra-low heavy metal content and consistent quality, it's ideal for critical medical and pharma applications.
- API (Active Pharmaceutical Ingredient) purification
- Injectable solution decolorization and depyrogenation
- Medical device and healthcare applications
- Hemoperfusion and medical treatment systems
- Compliant with USP, EP, and JP pharmacopeia standards
Food-Grade Purification Solutions
Our food-grade activated carbon meets strict quality standards for use in food and beverage processing. From sugar refining to edible oil processing, we deliver safe, effective purification solutions.
- Sugar decolorization and syrup purification
- Edible oil refining and bleaching processes
- Beverage clarification and taste improvement
- Food additive purification and processing
- Alcoholic beverage finishing and maturation
Need a Custom Application Solution?
Our technical team can help you find the perfect activated carbon solution for your specific application requirements.